


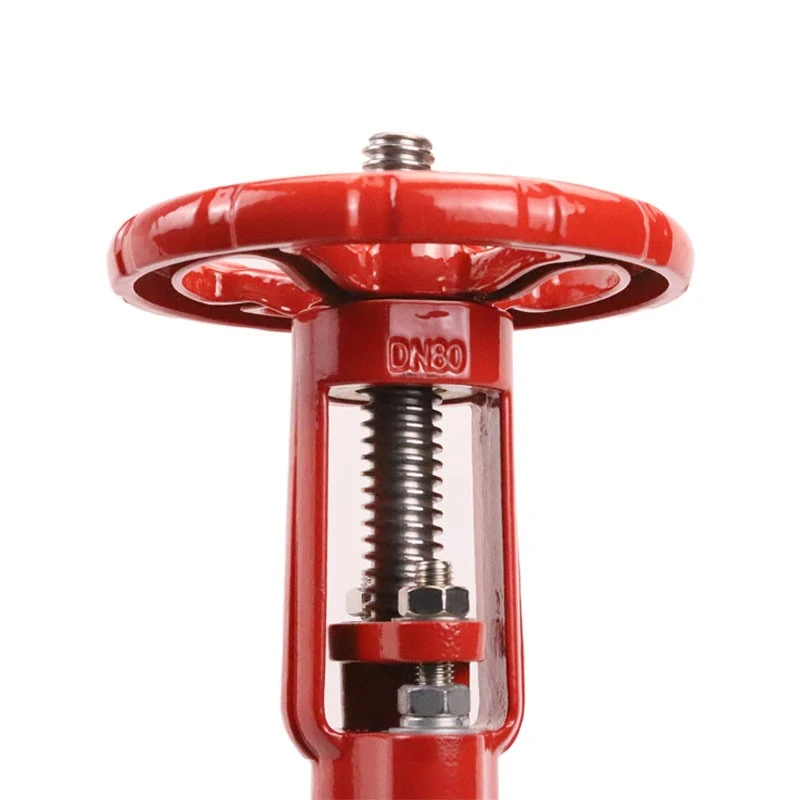


- Nonfir gate valves are engineered to meet strict FM Global fire protection requirements, delivering certified reliability and long-term performance for international fire protection systems.
- Nonfir gate valves are meticulously engineered to provide reliable performance in international fire safety projects. Each valve undergoes rigorous FM/UL testing to ensure fire resistance, leak-tight sealing, and rapid emergency response. By aligning with FM Global standards, Nonfir ensures seamless integration into global fire protection systems while delivering operational reliability and long-term durability.
|
Feature |
FM/UL Certified |
Non-Certified |
|
Certification |
FM Global fire protection / UL |
None |
|
Body Material |
High-strength cast / ductile iron |
Standard cast iron |
|
Stem Material |
Stainless steel, precision-machined |
Basic steel |
|
Sealing Performance |
Leak-proof under pressure |
Standard, may leak |
|
Operational Reliability |
Smooth after long idle periods |
Risk of sticking |
|
Testing & Verification |
Rigorous FM/UL testing |
Limited |
|
Applications |
Fire systems, industrial pipelines |
General, non-critical |
Product Details
Fire Protection Standards Explained
FM Global represents a benchmark for international fire safety compliance. Nonfir's gate valves are designed to satisfy critical criteria:
- Fire Resistance: Valve bodies and internal components withstand extreme temperatures, maintaining integrity under emergency conditions.
- Sealing Integrity: Precision-engineered sealing surfaces prevent leakage even under prolonged operation.
- Emergency Responsiveness: Optimized stem and opening mechanisms allow immediate activation when fire suppression is required.
Understanding these standards highlights the value Nonfir brings to engineers and contractors working on global fire protection projects.

Compliance Highlights of Nonfir Gate Valves
Nonfir gate valves combine high-quality materials, precise machining, and rigorous testing to meet international fire safety specifications:
- Durable Body Construction: Cast iron or ductile iron bodies provide strength while withstanding thermal stress.
- Stainless Steel Stem: Precision-machined stems resist corrosion and wear, ensuring smooth operation.
- Sealing Performance: Advanced EPDM or rubber seals guarantee tightness under high pressure and temperature.
- Certification Assurance: Each valve carries FM/UL certifications, providing verifiable quality and traceability.
This design philosophy ensures reliable valve operation in both building and industrial fire suppression systems.

Value for International Fire Protection Projects
Nonfir's adherence to fire protection standards offers tangible advantages for global projects:
- Global Compliance: Facilitates regulatory approval for international fire protection systems.
- Versatile Application: Suitable for commercial, industrial, and municipal fire protection pipelines.
- Operational Confidence: Maintains reliable performance under high-pressure and high-temperature conditions.
- Support & Documentation: Comprehensive technical guidance, dimensional drawings, and installation instructions are available to engineers worldwide.
Choosing Nonfir ensures that global projects maintain both safety and operational efficiency while complying with FM/UL standards.

FAQ
Q1: What does FM Global compliance mean?
A: It guarantees valves meet strict international standards for fire resistance, leak prevention, and operational reliability.
Q2: Are Nonfir valves suitable for international projects?
A: Yes, FM/UL certified valves are compatible with global fire protection systems and support project approvals.
Q3: How is emergency responsiveness ensured?
A: Precision stems and optimized valve mechanics allow immediate operation under high pressure during emergencies.
Q4: Can these valves remain idle without performance loss?
A: Yes, high-quality materials and design prevent sticking or degradation after long periods of inactivity.
Q5: What support does Nonfir provide for FM-certified installations?
A: Nonfir offers worldwide technical guidance, installation manuals, dimensional drawings, and responsive consultation.
Hot Tags: fm global fire protection, China fm global fire protection manufacturers, suppliers, factory, fire sprinkler system valve, Industrial Gate Valve, valves for fire fighting system, Gate Valve Stem, valves in fire fighting system, Gate Valve Dimensions


